Wholesale Custom Kitchen Cabinets
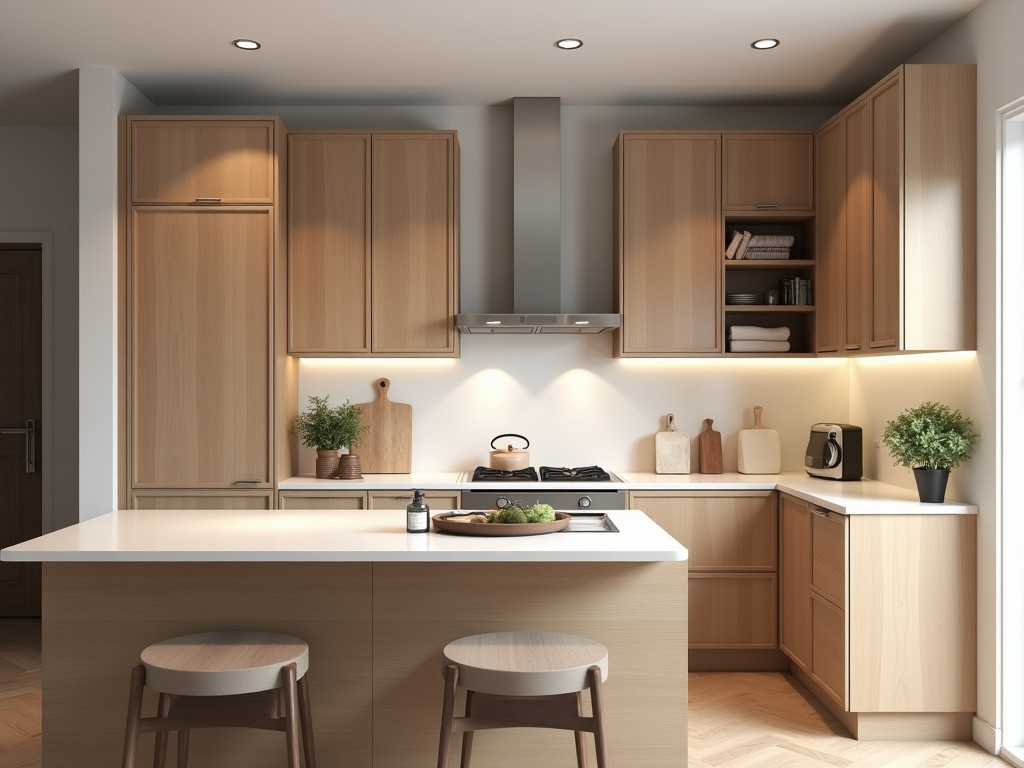
Wholesale Custom Kitchen Cabinets
Industrial buyers sourcing kitchen cabinetry for multi-unit residential, hospitality, or commercial projects require solutions that balance design flexibility with production efficiency. Wholesale
- Category:
- Kitchen Cabinet
Wholesale Custom Kitchen Cabinets
Industrial buyers sourcing kitchen cabinetry for multi-unit residential, hospitality, or commercial projects require solutions that balance design flexibility with production efficiency. Wholesale custom kitchen cabinets are manufactured to project-specific dimensions, finishes, and hardware specifications while maintaining consistent quality across large volumes. This approach reduces on-site modification needs and ensures dimensional compatibility with architectural plans.
Material Construction and Core Options
Cabinet carcasses are typically constructed from 16mm or 18mm engineered wood substrates selected based on load requirements and environmental exposure. Particleboard with melamine laminate offers cost-effective performance for dry interior applications, while moisture-resistant MDF or plywood cores are specified for high-humidity zones such as bathrooms or coastal installations. Edge banding is applied using hot-melt adhesive to seal substrate edges against moisture ingress and mechanical wear.
Door and drawer fronts utilize the same core materials but may incorporate additional surface treatments including thermofoil wrapping, UV-cured acrylic coatings, or wood veneer laminates. These finishes provide varying degrees of scratch resistance, color stability under UV exposure, and cleanability — critical factors in high-traffic environments. All surfaces are manufactured to meet ISO 2813 gloss standards and ISO 2409 adhesion test requirements.
Dimensional Customization and Modular Design
Unlike stock cabinets with fixed increments, wholesale custom units are built to exact opening dimensions provided by the client, eliminating filler strips and scribe molding. Standard base cabinet heights range from 720mm to 900mm to accommodate varying countertop thicknesses and accessibility requirements, while wall cabinets are typically manufactured between 300mm and 900mm in height with depths of 300mm or 350mm. All internal shelf positions are pre-drilled using CNC-guided systems to ensure alignment within ±0.5mm tolerance.
Customization extends to interior accessories such as pull-out trays, blind corner organizers, and vertical dividers, which are engineered to specific load capacities (typically 25kg–40kg per unit) and installed using concealed full-extension slides with soft-close mechanisms. Hardware mounting points are reinforced with metal brackets or threaded inserts to prevent pull-out under repeated use.
Production Tolerances and Quality Control
Dimensional accuracy is maintained through CNC nesting and drilling systems with positional repeatability of ±0.1mm. Panel squareness is verified using laser-guided alignment jigs during assembly, ensuring diagonal variance remains under 2mm per meter. All joints — whether cam-lock, dowel, or confirmat — are tested for torsional resistance to withstand dynamic loads from daily use without loosening over time.
Surface finish consistency is monitored via spectrophotometer readings to ensure ΔE<2 color variation across batches. Adhesion testing follows ASTM D3359 methodology, with minimum 4B rating required for all laminated surfaces. Edge banding undergoes peel resistance testing (ASTM D903) to confirm bond strength exceeds 1.5 N/mm before final packaging.
Packaging and Logistics for Bulk Orders
Finished cabinets are wrapped in 0.05mm polyethylene film to prevent surface abrasion, then placed in die-cut corrugated cardboard sleeves with corner protectors. Each unit is labeled with a unique barcode linking to its project-specific installation drawing, hardware pack, and assembly instructions. Palletized shipments use ISPM-15 compliant timber bases with stretch wrapping and edge bracing to withstand forklift handling and containerized transport.
Volume discounts apply based on total linear meters of cabinetry ordered, with tiered pricing structures typically beginning at 50lm for base pricing and increasing incrementally at 100lm, 250lm, and 500lm thresholds. Lead times are calculated per project but generally range from 3–6 weeks for standard materials and finishes, extending to 8–10 weeks for specialty veneers or custom color matches requiring laboratory formulation.
Applications in Commercial and Multi-Residential Projects
Wholesale custom cabinets are frequently specified in hotel guest rooms where dimensional consistency across hundreds of units ensures seamless installation and reduces warranty claims related to misalignment. In senior living facilities, cabinets are adapted with reduced-depth bases and elevated toe kicks to accommodate mobility aids while maintaining ADA-compliant reach ranges. Educational institutions specify chemical-resistant surfaces and locking mechanisms for laboratory or art classroom storage.
Retail environments utilize matching cabinet systems for back-of-house storage and customer-facing displays, requiring finishes that withstand frequent cleaning with alcohol-based sanitizers. Marine and offshore applications specify plywood cores with marine-grade adhesives and salt-resistant hardware to prevent delamination in high-humidity, saline conditions. Each application drives specific material and hardware selections based on environmental stressors and usage cycles.
| Component | Typical Specification | Customization Range |
|---|---|---|
| Cabinet Carcass Thickness | 16mm or 18mm | 12mm–25mm based on load |
| Door Overlay | Full overlay standard | Half inset, full inset available |
| Shelf Load Capacity | 20kg per shelf (uniformly distributed) | Up to 40kg with reinforcement |
| Hardware Finish | Nickel, chrome, matte black | Brass, bronze, custom PVD |
| Edge Banding Thickness | 0.5mm or 1.0mm PVC | Wood veneer, acrylic, ABS |
For project-specific quotations, provide architectural drawings, material preferences, hardware selections, and required delivery schedule. Our engineering team reviews submissions for manufacturability, identifies potential interference issues, and returns a detailed BOM with lead time confirmation within 2 business days. Contact us to initiate a technical review of your cabinetry requirements.



